News

  1. Home
  2. > News
Temperature cycling causes more leakage in O-Rings and Rubber Seals than fixed extreme temperatures, from dynamic coupled thermal damage. In Caoutchouc Industry and Rubber Processing, steady heat ages Rubber Products and creates compression set; low temperature shrinks Moulded Rubber Parts and Rubber Moulded Items. Repeated cycles cause irreversible damage and transient leakage for vehicle and pipeline Industrial Seals. Rings, Gaskets and Silicone Gaskets rely on compressive contact pressure. Synthetic Rubbers (EPDM Rubber, Silicone Rubbers) expand more than metal grooves. Temperature cycling changes Rubber Parts’ compression ratio. Thermal expansion and cold hardening reduce resilience of Car Rubber Gaskets, Rubber Seals for Fittings and Silicone Foam Seals. High-temperature: Overexpanded Rubber over-compresses O-Rings and Gaskets. Aging triggers compression set and stress relaxation. Cooled Moulded Rubber Parts lose rebound, leading to permanent seal damage. Low-temperature: Synthetic Rubbers shrink and stiffen. Rubber Products fail to regain elasticity on cold startup, causing pressure-induced transient leakage. Cumulative cyclic damage: Thermal cycles degrade Industrial Seals via over-compression, falling sealing force, interfacial slip and crack growth, eventually failing Car Rubber Gaskets and Rubber Seals for Fittings. Thermal shock & system risks: Mismatched deformation between Rubber Parts and metal cracks or peels Seal Rings. Structural distortion and pressure-temperature coupling speed up failure, also affecting Rubber Hoses, Bellows and Rubber Buffers. Failure scenarios & controls: Leakage occurs during cold startup, thermal shock and low-pressure gas/vacuum. For Moulded Rubber Parts Manufacture, select rubbers with good low-temp and anti-ageing performance, optimize groove compression and structure, and run real thermal cycle tests to ensure Rubber Products reliability.
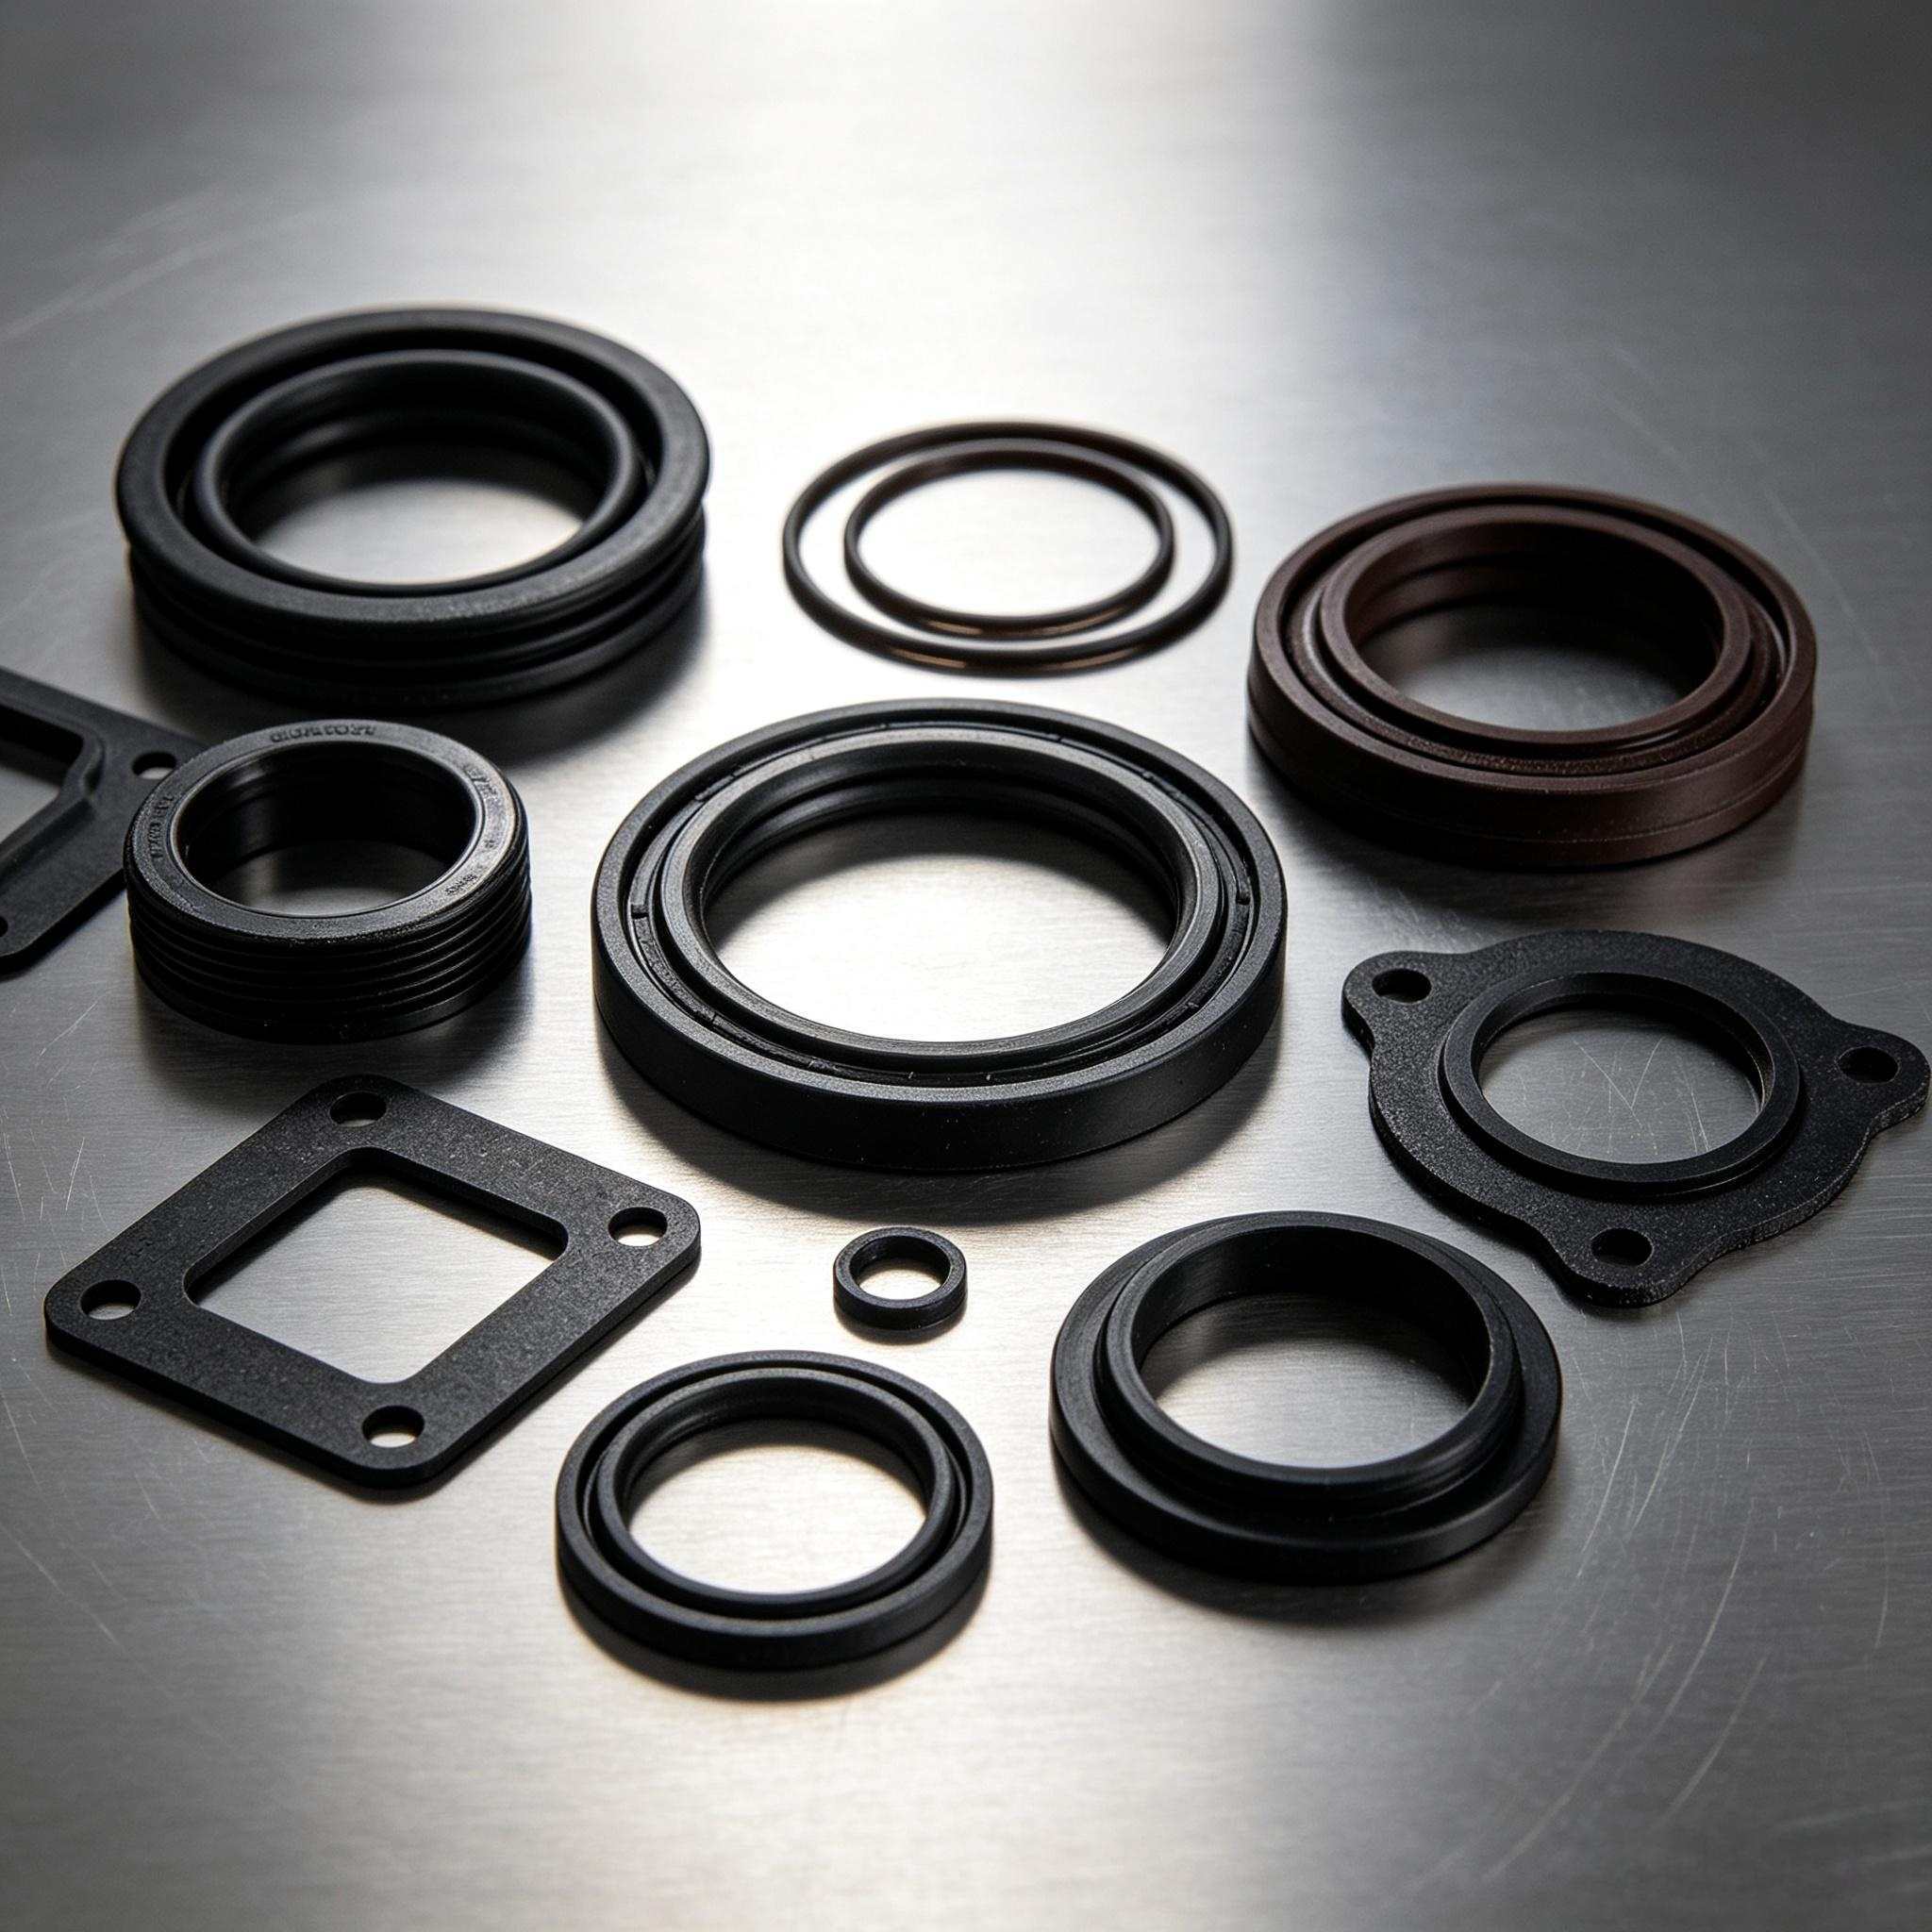
Most seal failures come from wrong material selection. For seal rings, gaskets, O-rings & industrial seals, check 3 conditions: Medium: mineral oil, water, brake fluid, acid/alkali. Wrong material swells or cracks (for rubber parts, moulded rubber parts, car rubber gaskets). Temperature: continuous working temp, not peak heat. Overheating reduces lifespan of rubber seals for fittings, rubber hoses, bellows. Seal type: dynamic seals need wear resistance; static seals depend on compression recovery. NBR:Standard for hydraulic/lubrication systems, -30~100℃, good mineral oil resistance. Widely used for rubber products, industry rubber. Weak against ozone, aromatics and ketones. EPDM Rubber:Great for hot water, steam, DOT3/DOT4 brake fluid, excellent weather resistance. Critical: Incompatible with mineral oil, leads to severe swelling. FKM:High temperature & chemical resistance up to 200℃+, ideal for engines, pumps and oilfield equipment. Higher cost; poor low-temp performance, not compatible with ketones/esters. VMQ (Silicone):Wide temp range -60~200℃, FDA grades available. Used for silicone gaskets, silicone foam seals. Low tensile strength, unsuitable for dynamic sealing; swells in mineral oil. HNBR:Modified NBR. Oil resistant, continuous temp up to 150℃, better wear & ozone resistance. Mid-cost option for automotive & oilfield moulded rubber items. PTFE:Not an elastomer. Outstanding chemical resistance, wide temperature range and low friction. Lacks elasticity; used for spring energized seals or coating over rubber substrates. NBR for mineral oil; FKM/HNBR for high-temp harsh conditions; EPDM for water, steam & outdoor service; VMQ for food-grade static sealing; PTFE for heavy corrosion. These elastomers are key materials in rubber processing and caoutchouc industry, used to produce rubber buffers, rubber metal buffer, elastic bands and rubber moulded items. Select proper synthetic rubbers or silicone rubbers by checking medium, temperature and seal type.
Same material, different lifespan. EPDM performance varies greatly. Its durability relies on formula, hardness, compression rate, groove geometry, medium and temperature. Long-term compression set and ageing resistance outweigh nominal single-point parameters. Composite sealing becomes the new trend. Fillers, blending and surface coatings balance conflicting performance requirements. Sealing has evolved from individual components into multi-material, self-compensating structural systems. Material iteration defines valve application boundaries. Every upgrade of sealing materials extends valves’operating range for temperature, pressure, corrosion and cyclic service, supporting extreme industrial working conditions. Sealing evolves from accessory to core technology. The traditional design mindset that prioritizes valve body then selects seals is outdated. Sealing systems govern valve torque, tightness, service life and media compatibility. Sealing is systematic engineering. Most seal failures stem from mismatched structure, clearance and operating conditions instead of defective raw materials. Reliable sealing demands proper coordination among material, structure and service environment. Sealing details differentiate high-end valves. Valve bodies share similar construction. Product gaps hide in unseen sealing design: material grading, compound formula, compression ratio and groove precision.   Five future directions for sealing technology. Advanced composites, data-backed material selection, surface coating, additive manufacturing and intelligent monitoring shift seals from passive endurance to active condition control. Core industry insight. The evolution of sealing materials fuels industrial advancement. Future competition in valve industry lies in optimized matching of material, structure and working conditions, rather than simply specifying costly premium materials.
Reliable valve operation hinges on seals. From natural substances to synthetic rubber, PTFE, graphite and metal composites, sealing materials have continuously expanded valves’ limits of temperature, pressure and chemical resistance. 1st revolution: Natural materials for gap sealing. Early practitioners used hemp, cotton, leather and beeswax to block clearances between rigid components and stop basic leakage. This established the core logic of flexible packing, still adopted by packing seals today. 2nd revolution: Rubber delivers elastic industrial sealing. Natural rubber features compressibility and resilience to compensate for dimensional tolerances of parts. It brought about O-rings and rubber gaskets. Sealing evolved from simple gap filling to sustained sealing force generated by elasticity, enabling engineered design. 3rd revolution: Synthetic rubber for diverse service conditions. Natural rubber suffers poor oil resistance and ageing performance. NBR resists mineral oil; EPDM suits aqueous media; FKM withstands high-temperature chemicals. A core rule was formed: material selection must match medium, temperature and pressure. NBR and EPDM cannot be swapped arbitrarily. Though visually similar, they differ greatly in chemical resistance. Interchangeable assembly may work temporarily, yet swelling, loss of elasticity and leakage will occur over time. Seal selection prioritises long-term stability under working conditions, not static test data. 4th revolution: PTFE ushers in the low-friction era. With low friction and excellent chemical resistance, PTFE is widely used in ball valve seats and gaskets, greatly cutting valve operating torque. Its downside is creep and cold flow, driving material modification. Filled PTFE shifts from single material to custom formulation. Fillers such as glass fibre, carbon fibre and graphite improve its creep resistance and wear performance. PTFE grades vary drastically with different fillers, making custom formulation a key development direction. 5th revolution: High-performance engineering plastics emerge. High-strength materials like PEEK and PPS handle high-temperature, high-pressure and abrasive conditions for premium valve seats and sealing assemblies. Higher cost does not equal better performance; selection balances service requirements and cost. 6th revolution: Multi-material combined sealing. Metals provide rigidity, engineering plastics offer wear-resistant support, and elastomers absorb deformation. Seal design no longer relies on one single material, but a coordinated material system. 7th revolution: Graphite breaks high-temperature limits. Flexible graphite offers high heat resistance and decent resilience, used for high-temperature valve stem packing and flange gaskets. The industry adopted temperature-based material selection. 8th revolution: Focus on medium compatibility. For demanding chemical, pharmaceutical and other services, chemical resistance becomes critical. Seals are no longer ordinary purchased parts; immersion and life tests are required to verify medium compatibility. 9th revolution: Upgrade from static tightness to dynamic reliability. Repeated opening/closing causes friction and wear, making dynamic sealing more challenging. Design predicts service life by integrating material, structure and motion parameters. 10th revolution: The ultra-low leakage era. Modern industry imposes strict limits on trace leakage. Sealing performance depends on the whole system. Full-process control from material, tolerance, machining to assembly is required, rather than only final inspection. The evolution of sealing materials mirrors the advancement of industrial equipment. Competition in valve industry is no longer about material cost alone, but the precise matching and systematic optimisation of material, structure and working conditions.
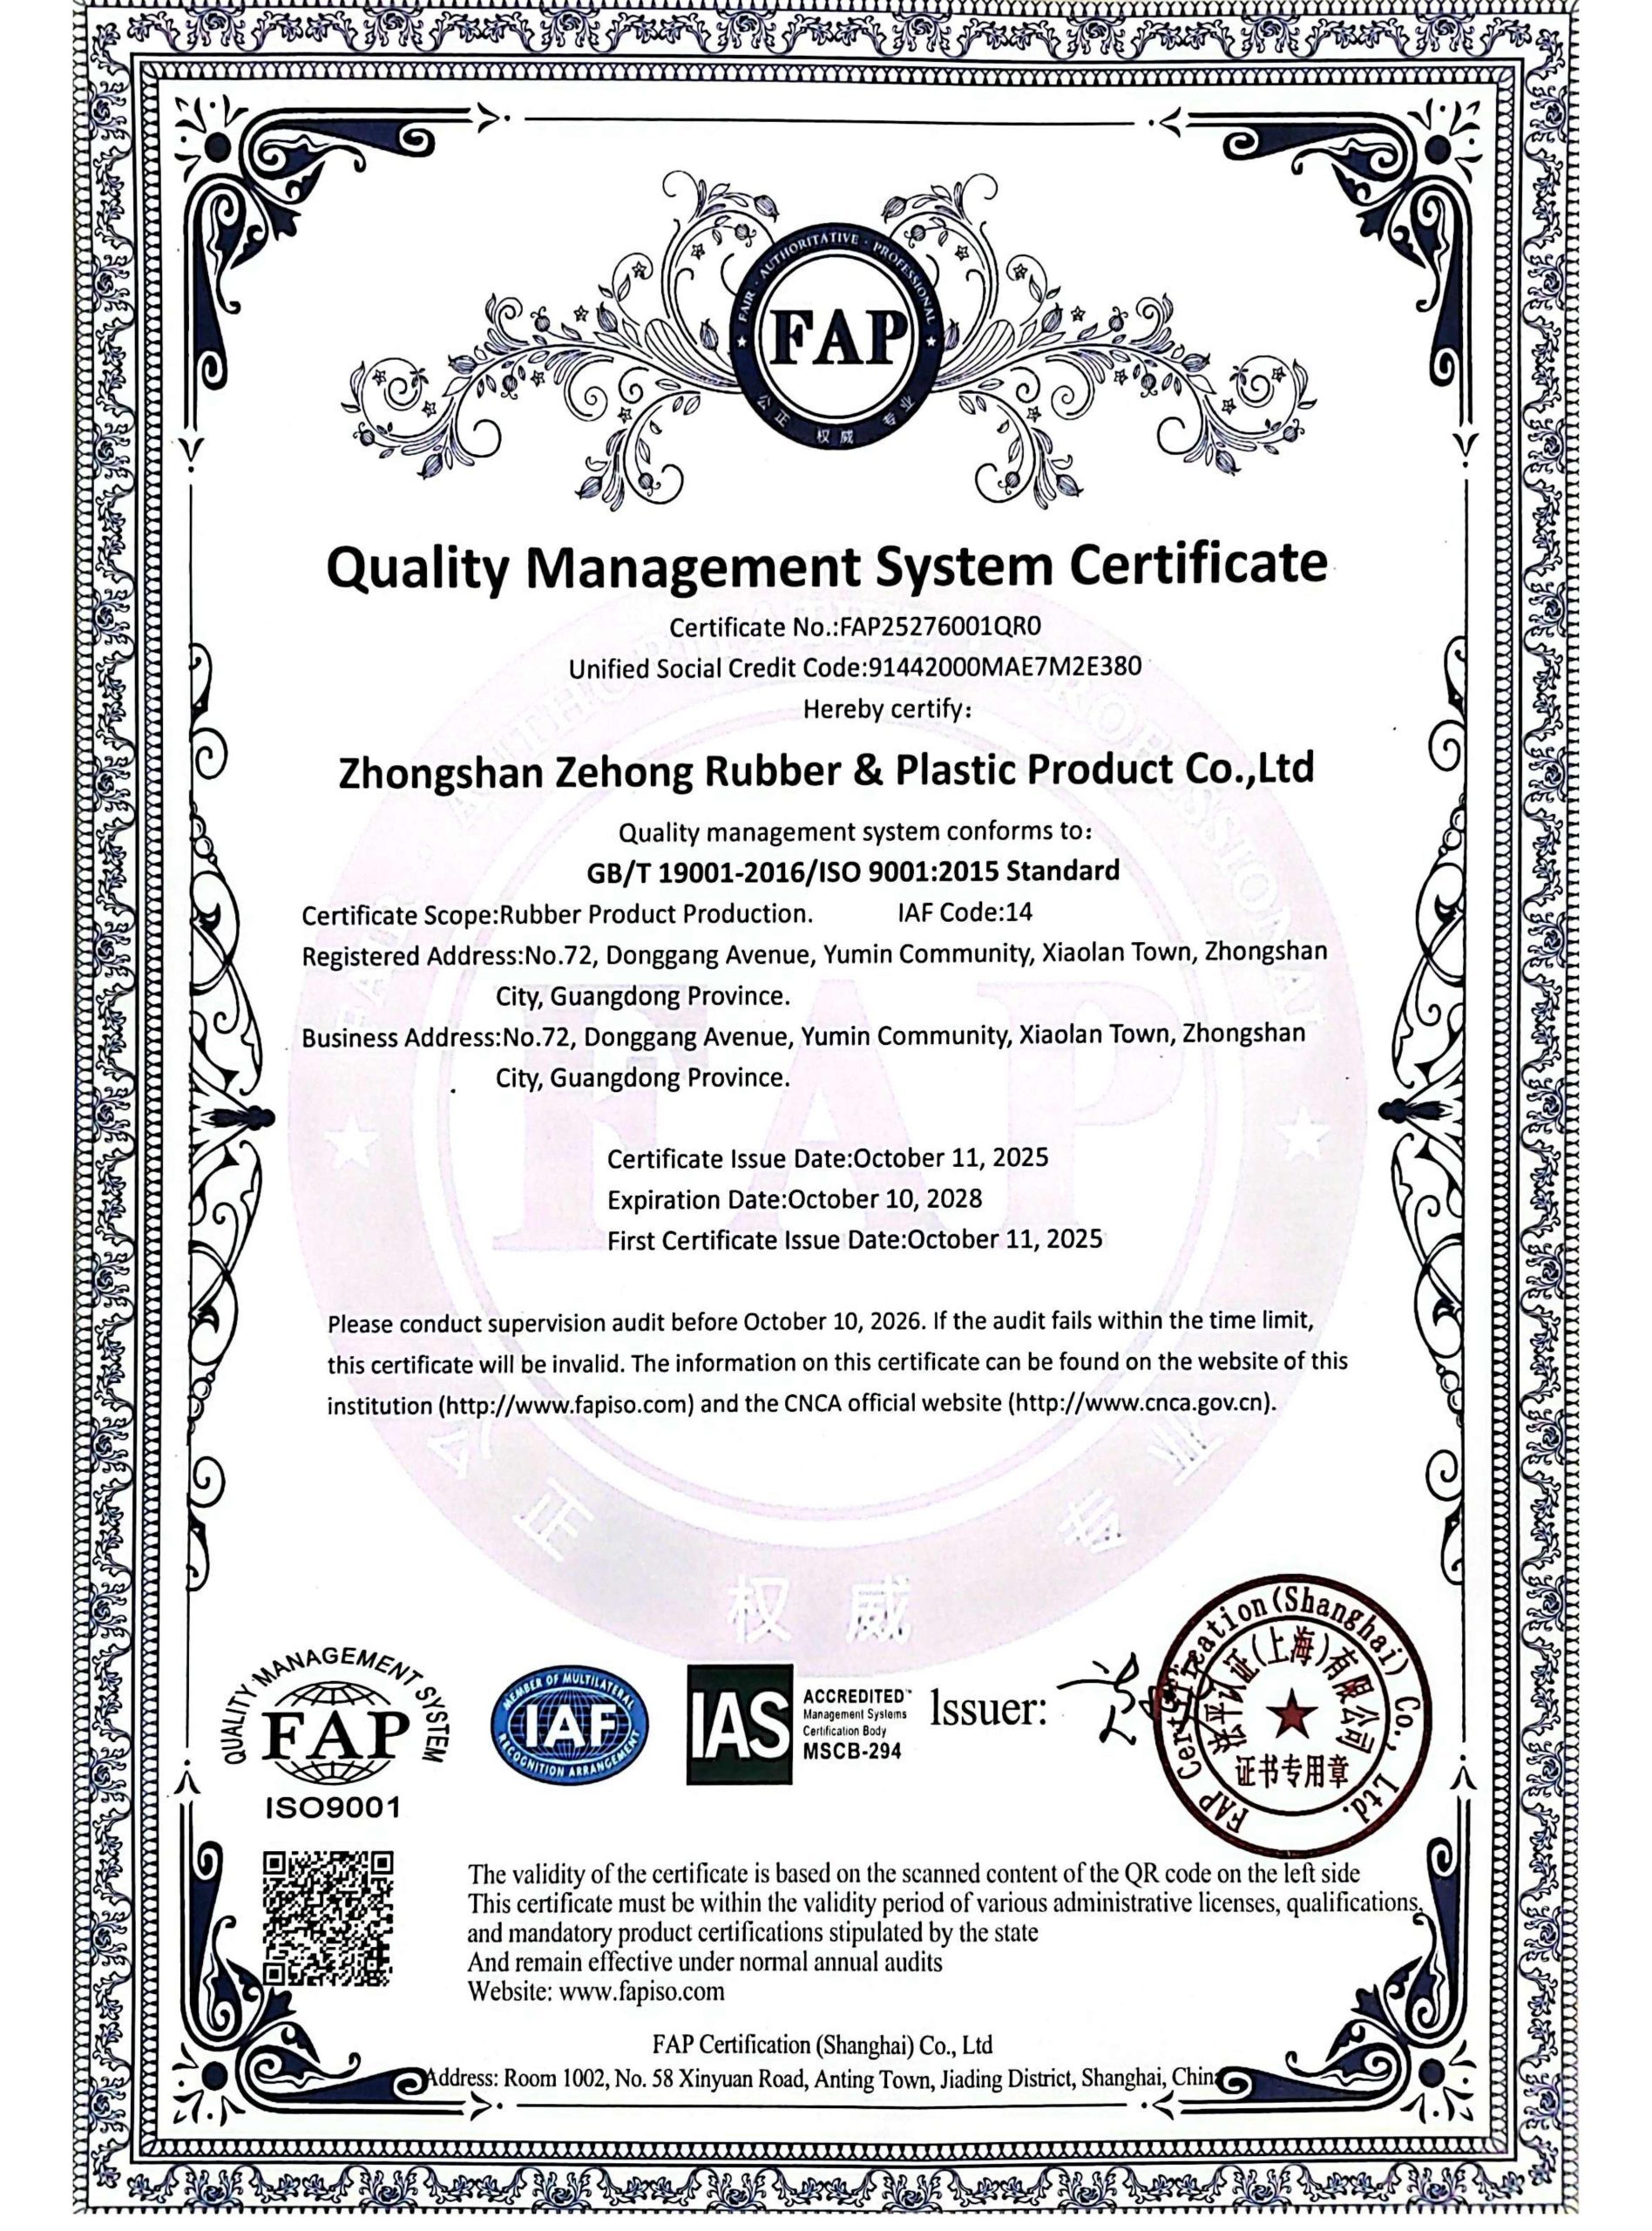
Our company has officially obtained the ISO9001:2015 Quality Management System Certification on October 11, 2025. This certification fully validates our standardized manufacturing and quality control systems for industrial rubber and silicone products, including gaskets, O-rings, rubber seals, silicone gaskets, EPDM rubber parts and moulded rubber components. It confirms that our entire production process complies with international industrial quality standards for sealing solutions and custom rubber manufacture. Specializing in industrial seals, moulded rubber items and caoutchouc product processing, we implement strict quality inspection from raw material verification, precision moulding, production supervision to finished product testing. Every industrial rubber and silicone component is produced under stable, traceable and standardized quality management. With the official ISO9001 certification, we further guarantee stable performance, reliable sealing quality and consistent delivery for all custom OEM and ODM rubber and silicone products, serving global industrial clients with trustworthy manufacturing solutions.
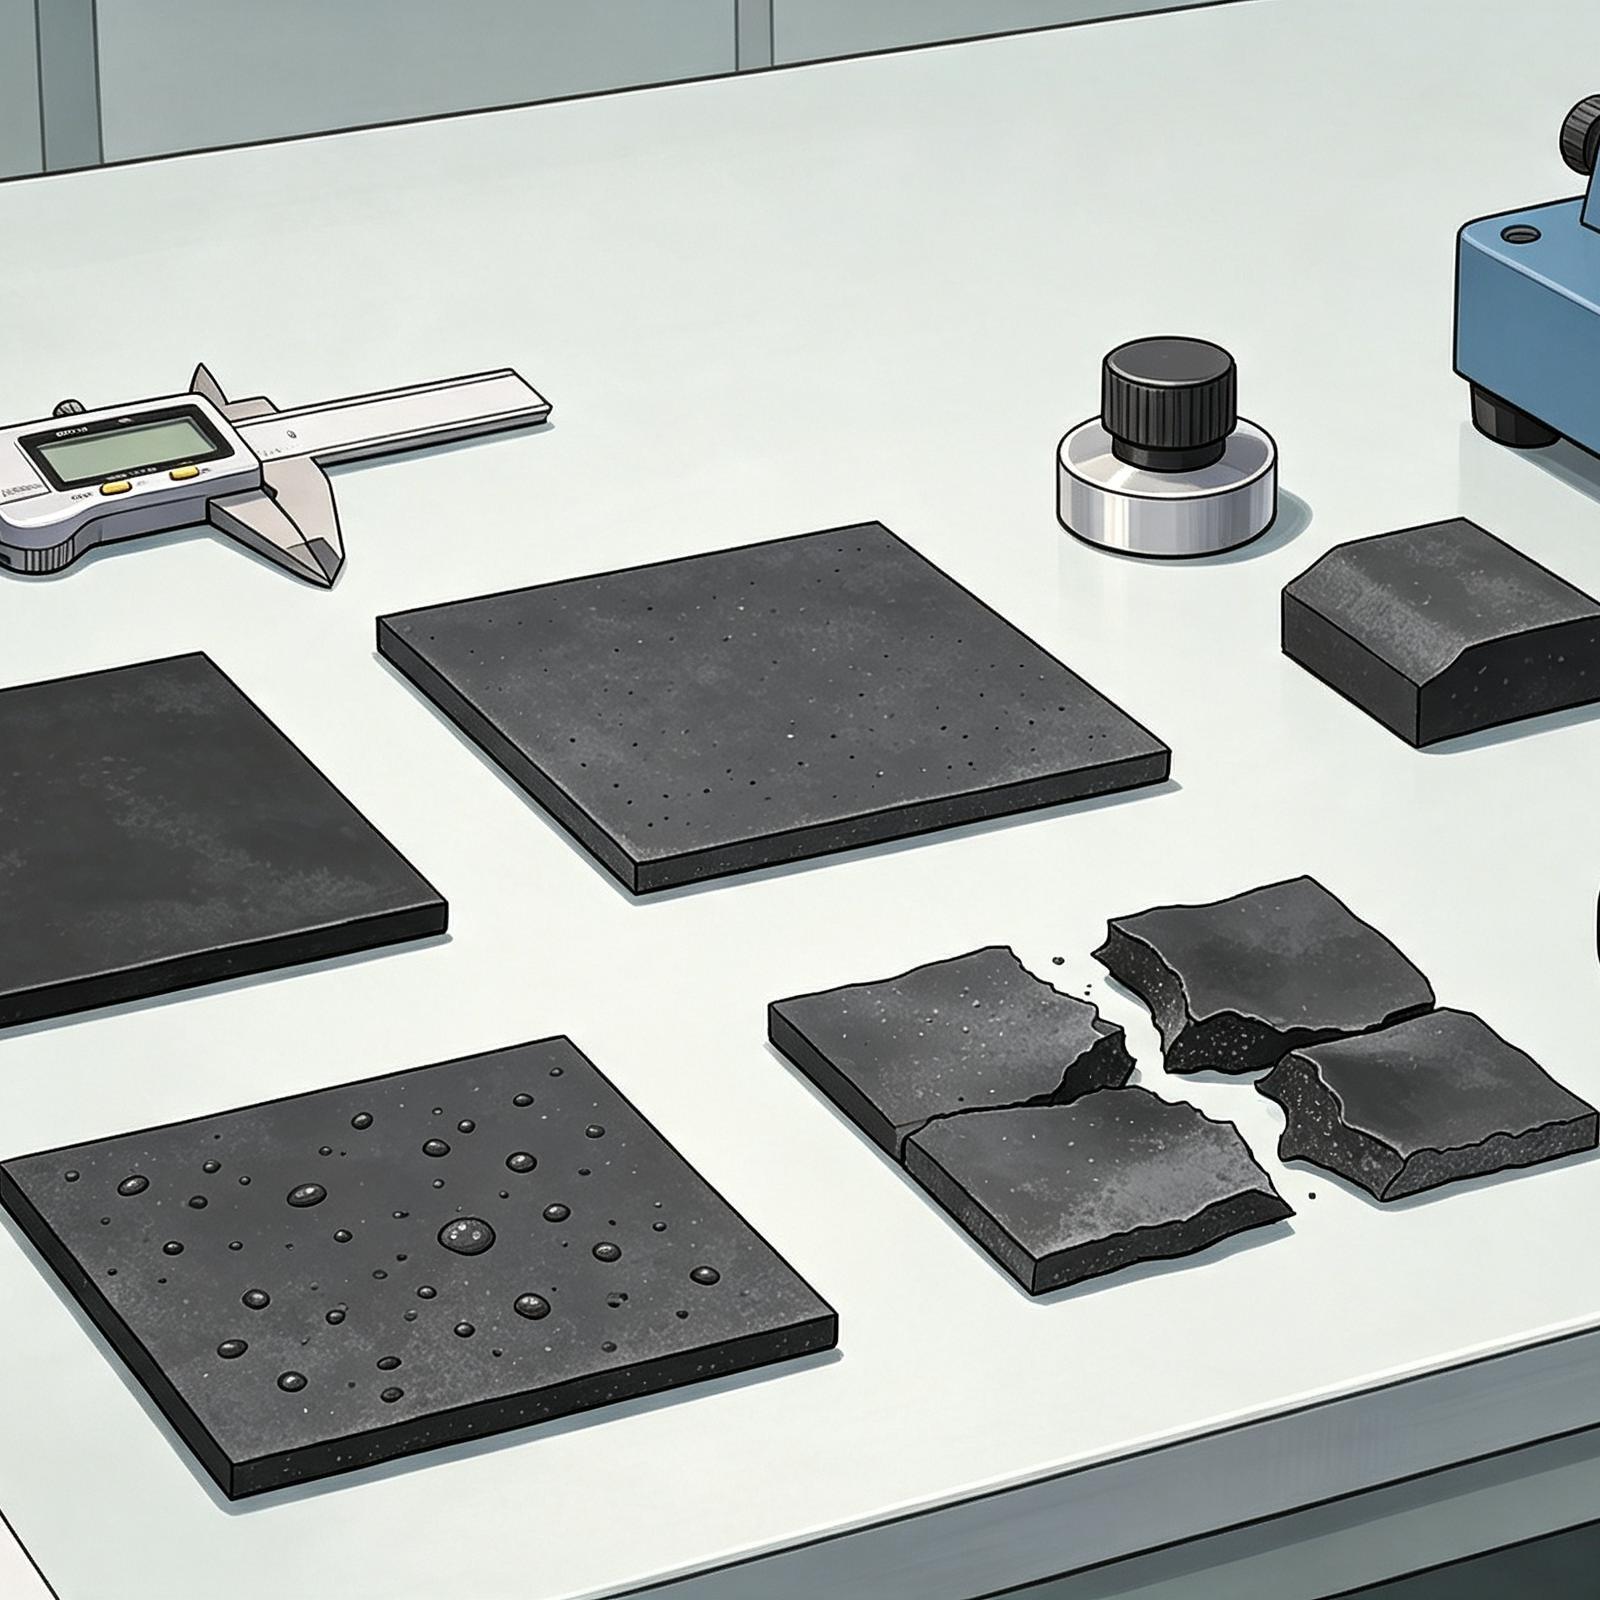
I. Four Major Causes of Uneven Rubber Mixing Uneven mixing cannot be simply attributed to operators’ negligence. The root causes cover formula design, processing, equipment and raw materials, categorized into four types as below: I. Four Major Causes of Uneven Rubber Mixing Uneven mixing cannot be simply attributed to operators’ negligence. The root causes cover formula design, processing, equipment and raw materials, categorized into four types as below: 1. Hardness Property fluctuation across one single part is obvious. High carbon black accumulation creates hard zones while filler-deficient areas stay soft, leading to customer rejection during QC inspection. 2. Tear Strength (Top Failure Indicator for Uneven Mixing) Undispersed filler agglomerates form internal stress concentration points. Tiny surface cracks expand rapidly under force, resulting in easy tearing. 3. Tensile Strength & Elongation at Break Disordered filler networks fail to uniformly bind rubber molecular chains. Localized fracture occurs under tension, causing sharp decline in tensile test readings. 4. Compression Set Unevenly dispersed curatives (sulfur, accelerators) cause partial overcure (brittle sections) and undercure (tacky sections). Inhomogeneous crosslink networks ruin long-term resilience of seals like O-rings, which cannot rebound after compression. 5. Dynamic Heat Build-up & Flex Fatigue Life Repeated compression generates severe friction heat inside carbon black aggregates (the Payne Effect). Trapped internal heat triggers thermal degradation, causing premature cracking of shock pads and tires under cyclic motion. 6. Surface Appearance Defects include pits, flow marks and peeling on molded parts. Excess blooming or oil bleeding occurs after storage, as clustered additives exceed rubber’s solubility limit and migrate outward.